INDUSTRIES
ROCOM designs and delivers bulk material handling and powders processing systems that keep materials moving efficiently. From hygienic food and dairy applications to wear-resistant building materials and recycling plants, we reduce dust, bottlenecks and downtime.
See all Industries
Chemicals & Fertilizers
Corrosion-resistant, dust-tight systems for handling urea, NPK, potash, phosphates and chemical additives.
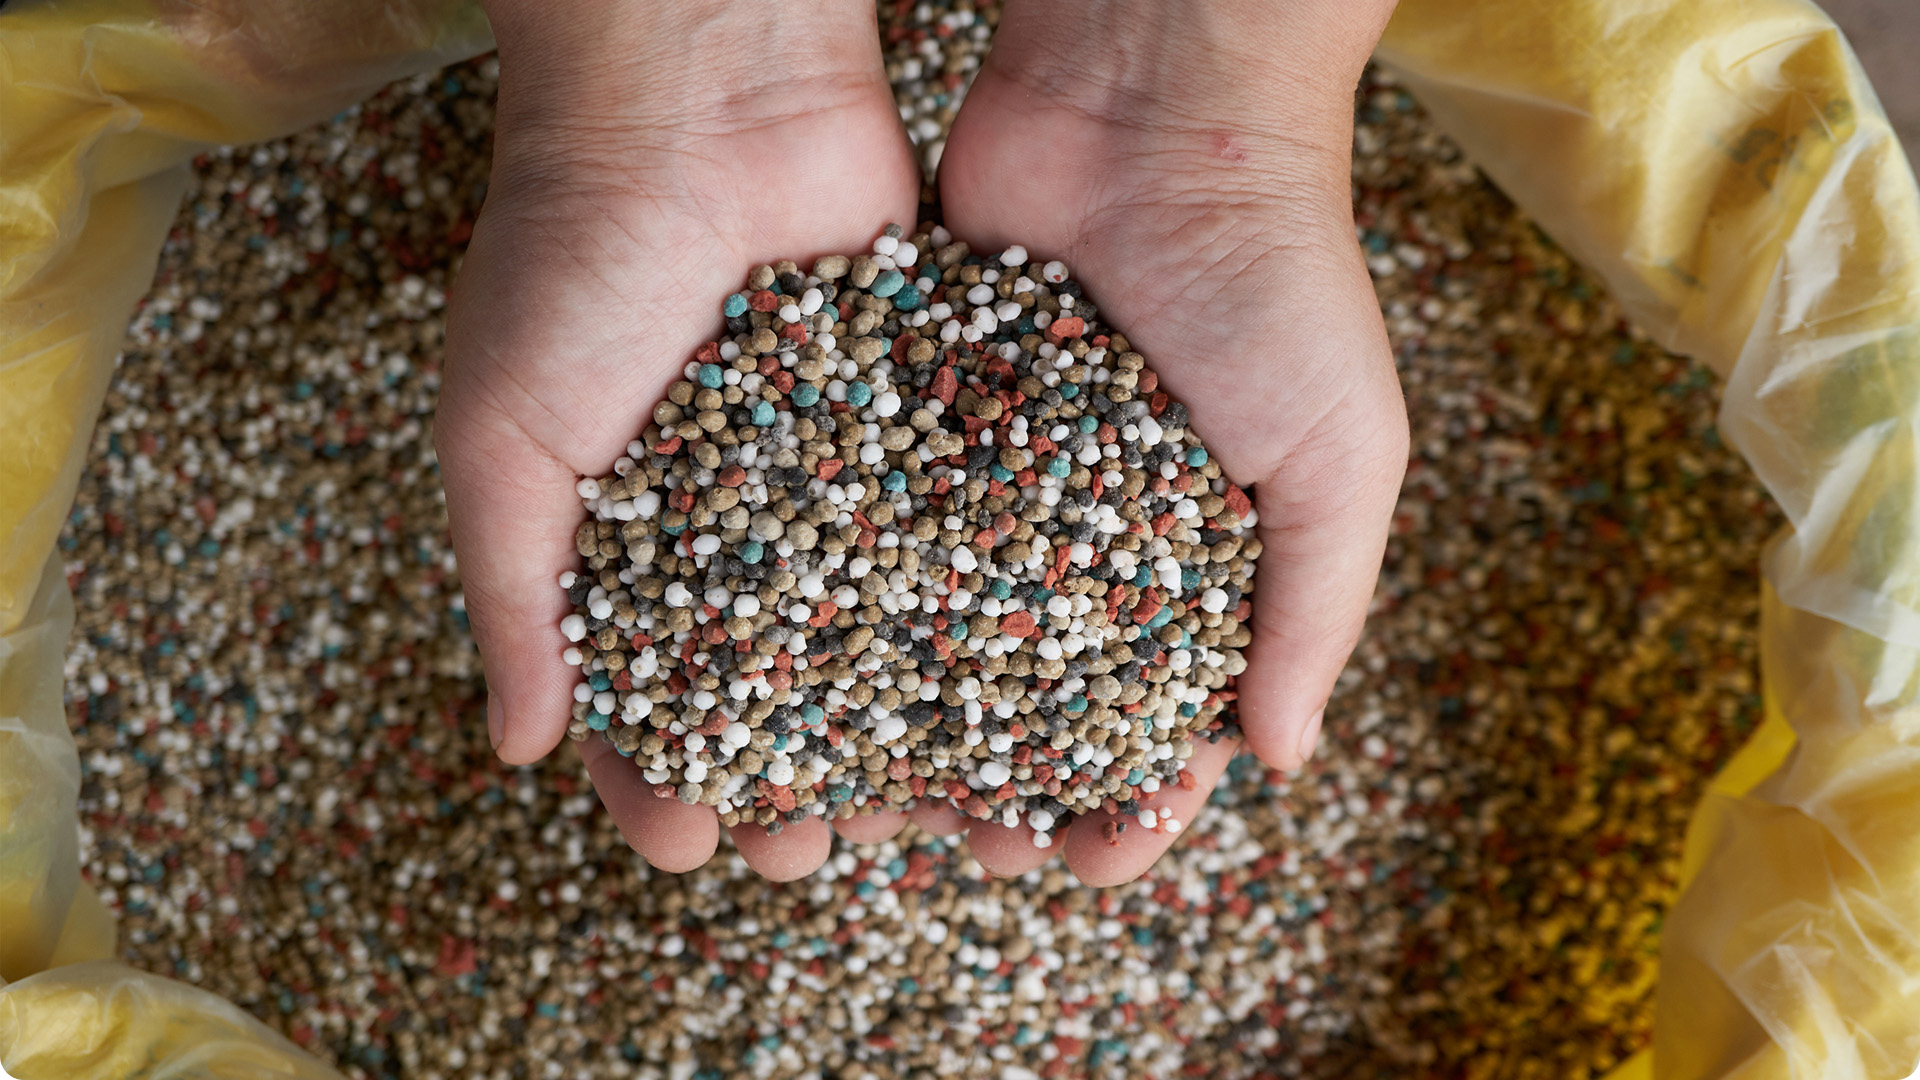
Material handling equipment for the chemical industry and fertilizer processing must safely manage corrosive, hygroscopic, abrasive and potentially hazardous bulk solids. ROCOM provides solutions for urea, NPK, potash and phosphate handling, including corrosion-resistant conveying systems, anti-caking vibrating screens, loss-in-weight feeders and controlled bulk solids handling equipment.
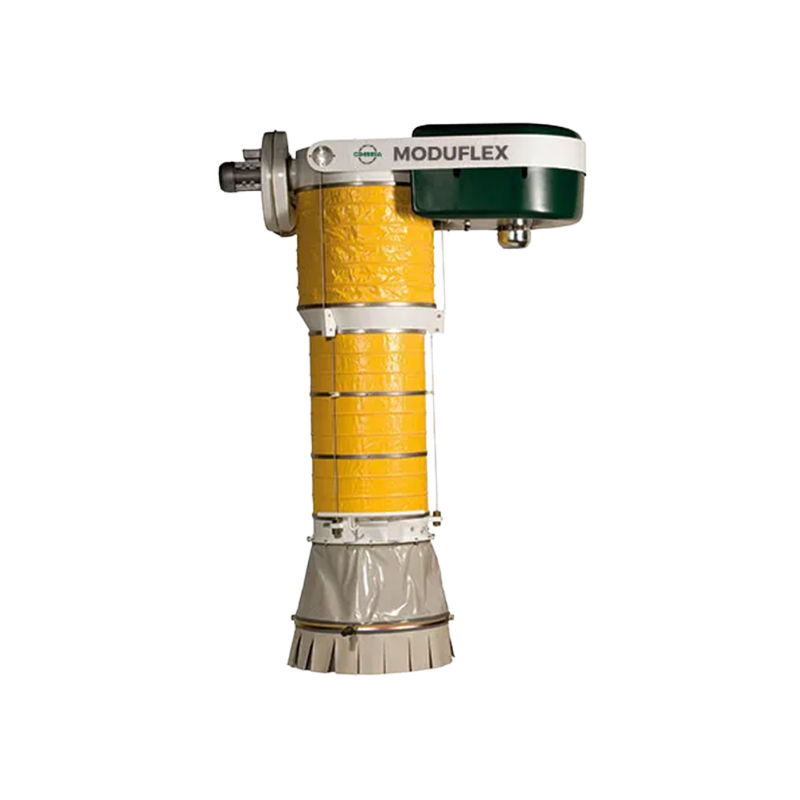
Big bag filling and unloading stations support contained material transfer, while dust-free telescopic loading chutes reduce product loss and environmental dust during vehicle loading. Enclosed conveying, accurate dosing and appropriate material selection help limit caking, corrosion and chemical degradation. Where explosive atmospheres may occur, ATEX conveying equipment supports safer operation through dust containment, grounding and suitable explosion-risk mitigation measures.
Materials and Handling Challenges We Solve
Bulk materials we handle include urea, NPK fertilizers, potash, phosphates, technical salts, mineral additives and fine chemical powders. These products may absorb moisture, cake, corrode equipment, generate dust or cause abrasive wear during conveying and dosing. Our solutions are selected to maintain stable flow, reduce blockages and product loss, protect operators and equipment, and support safer, cleaner and more reliable processing.
Corrosion-Resistant Conveying & Specialized Piping
Mechanical & Pneumatic Conveying Systems
For safe, enclosed transport of volatile or hazardous chemical powders, our dust-tight pneumatic conveying systems isolate materials from ambient moisture, preventing caking and ambient emissions. For high-volume fertilizer crystals, we supply robust mechanical conveying lines to maintain high mass-flow rates.
Wear & Corrosion Protection Piping
Chemicals like potassium chloride and compound fertilizers are both highly abrasive and chemical-aggressive. We utilize stainless steel alloys, special polymer liners and wear protection piping components to shield system internals from simultaneous corrosive and erosive attack, drastically extending pipe infrastructure lifespans.
Slide Gates, Rotary Valves & Diverters
Engineered for precise flow isolation beneath silos and hoppers, our specialized slide gates and rotary valves utilize advanced air-purged seals and corrosion-proof contact materials to meter raw chemicals safely. High-efficiency diverter valves allow seamless routing of material streams to different production or storage vessels while maintaining system air pressure differentials.
Classification, Quality Protection & Precision Dosing
Vibrating Screens for Anti-Caking
To guarantee product quality prior to packaging, our heavy-duty vibrating screens remove lumps, oversize crusts and fine dust generated during chemical storage or fluid-bed drying, ensuring a perfectly uniform particle size distribution.
Weighing, Dosing & Feeding Equipment
For complex blending recipes (such as NPK fertilizer compounding), our high-precision loss-in-weight feeders and weighing equipment provide continuous, highly accurate chemical dosing, preventing recipe drifting and maintaining strict process compliance.
Magnetic Separation Quality Control
To ensure absolute chemical purity and protect downstream milling machinery, we position high-intensity inline magnetic separators to continuously capture iron contaminants and scale from raw chemical feedstocks.
Sealed Containment & End-of-Line Packaging
Big Bag Filling & Emptying Units
Handling raw chemicals in FIBC bulk bags requires high safety standards. Our emptying stations feature integrated dust-extraction hoods and pneumatic massage paddles to reliably discharge poor-flowing or compacted powders. Our filling units combine inflatable neck seals with automatic weighing to prepare stable, dust-free bag shipments.
Telescopic Loading Chutes
For bulk logistics via tanker trucks, railcars or vessels, our telescopic loading chutes extend directly into the vehicle hatch. Integrated air extraction prevents fugitive chemical dust from escaping into the environment during high-speed gravity discharging.
Moisture-Proof Packaging, Palletizing & Wrapping
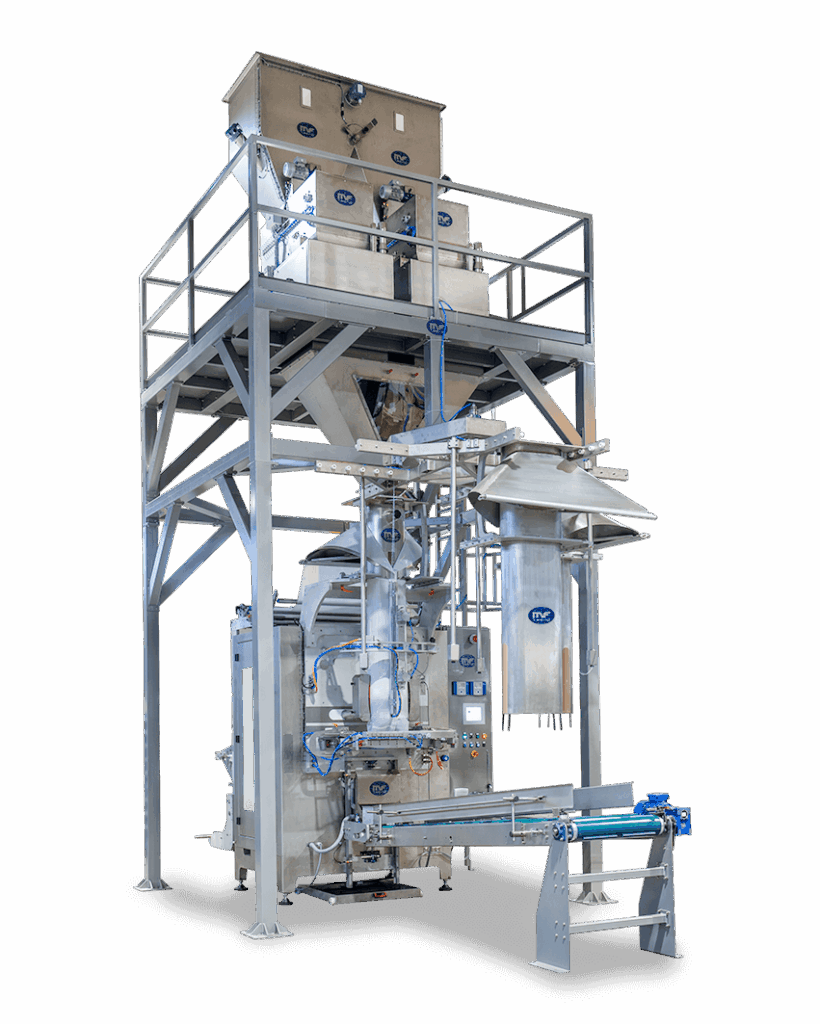
Corrosive and hygroscopic chemicals require airtight protection. Our automated bagging and packaging lines seal finished products into moisture-proof, plastic bags. These are automatically stacked by palletizers into stable loads, which are then secured by automated stretch-wrapping or stretch-hooding machines, providing a completely weatherproof seal for long-term storage and ocean transit.
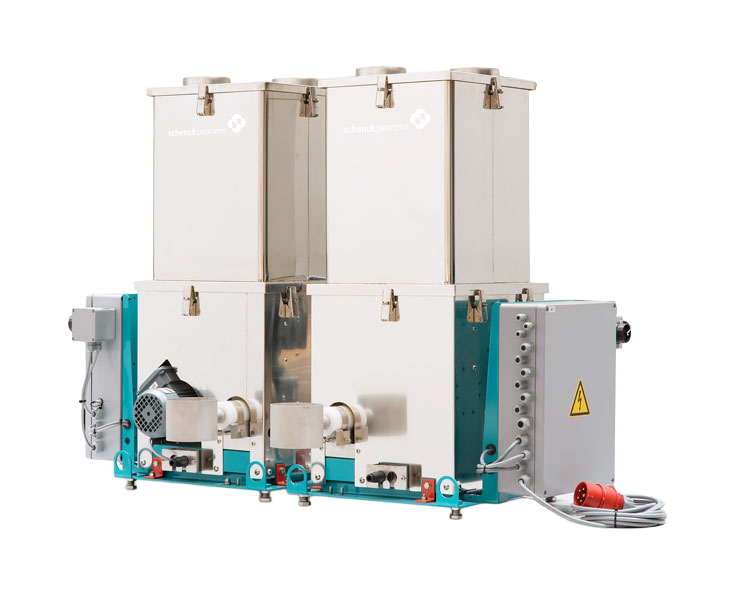
Bulk Handling Technologies for Chemical & Fertilizers
- Magnetic Separation Equipment
- Slide Gate Valves
- Rotary Valves
- Vibrating Equipment
- Weighing & Feeding Systems
- Dust Filters & Industrial Vacuum Cleaners
- Mechanical & Pneumatic Conveying
- Filling & Emptying Systems
- Loading Chutes
- Packaging, Palletizing & Wrapping Systems
Frequently Asked Questions
What is chemical & fertilizer handling equipment?
Chemical and fertilizer handling equipment is the set of conveying, screening, dosing, separation, containment and packaging systems used to move and process corrosive, hygroscopic and dust-prone bulk solids — such as urea, NPK compounds, potash, phosphates and chemical additives — safely through a plant. Because these materials are aggressive and often hazardous, the equipment uses corrosion-resistant materials, dust-tight enclosures, air-purged seals and (where required) ATEX-rated components to prevent caking, contamination, emissions and degradation.
How do you handle corrosive and hygroscopic chemicals without caking or degradation?
We isolate the material from ambient moisture with dust-tight pneumatic conveying and sealed transfer points, line piping and high-wear zones with stainless alloys or polymer liners, and remove lumps and crusts with anti-caking vibrating screens before packaging. Moisture-proof bagging and wrapping then protect the finished product through storage and transit.
What equipment is used to dose and blend fertilizers like NPK accurately?
Continuous loss-in-weight (gravimetric) feeders and weighing equipment meter each component to recipe, preventing drift in NPK and compound-fertilizer blending. Combined with slide gates, rotary valves and diverters for clean flow isolation, this keeps dosing accurate and the process compliant.
How is dust controlled when loading chemicals and fertilizers into trucks or rail?
Telescopic loading chutes extend into the truck, railcar or vessel hatch and use integrated dust extraction so fugitive chemical dust is captured rather than released during high-speed gravity loading. Inside the plant, dust-tight conveying, sealed big-bag stations and filtration keep emissions contained.
Can the equipment be made ATEX-compliant for hazardous chemical dust?
Yes. Where chemical or fertilizer dust is combustible or the area is zoned, ROCOM provides ATEX-rated rotary valves, vacuum/conveying components and controls, plus air-purged seals and grounded, dust-tight enclosures, so the system meets the site's explosion-protection requirements.
Our Partners

Contact Us
We look forward to discussing with you!