INDUSTRIES
ROCOM designs and delivers bulk material handling and powders processing systems that keep materials moving efficiently. From hygienic food and dairy applications to wear-resistant building materials and recycling plants, we reduce dust, bottlenecks and downtime.
See all Industries
Food & Dairy
Hygienic, ATEX-compliant systems for conveying, screening, dosing, separating and packaging food and dairy powders.
Handling infant formula, milk powder, whey, sugar, starch and spices calls for hygienic powder handling systems that protect product safety, ensure accurate dosing and maintain reliable flow. These fine organic powders can retain residues, support bacterial growth, cause allergen cross-contamination and form combustible dust clouds.
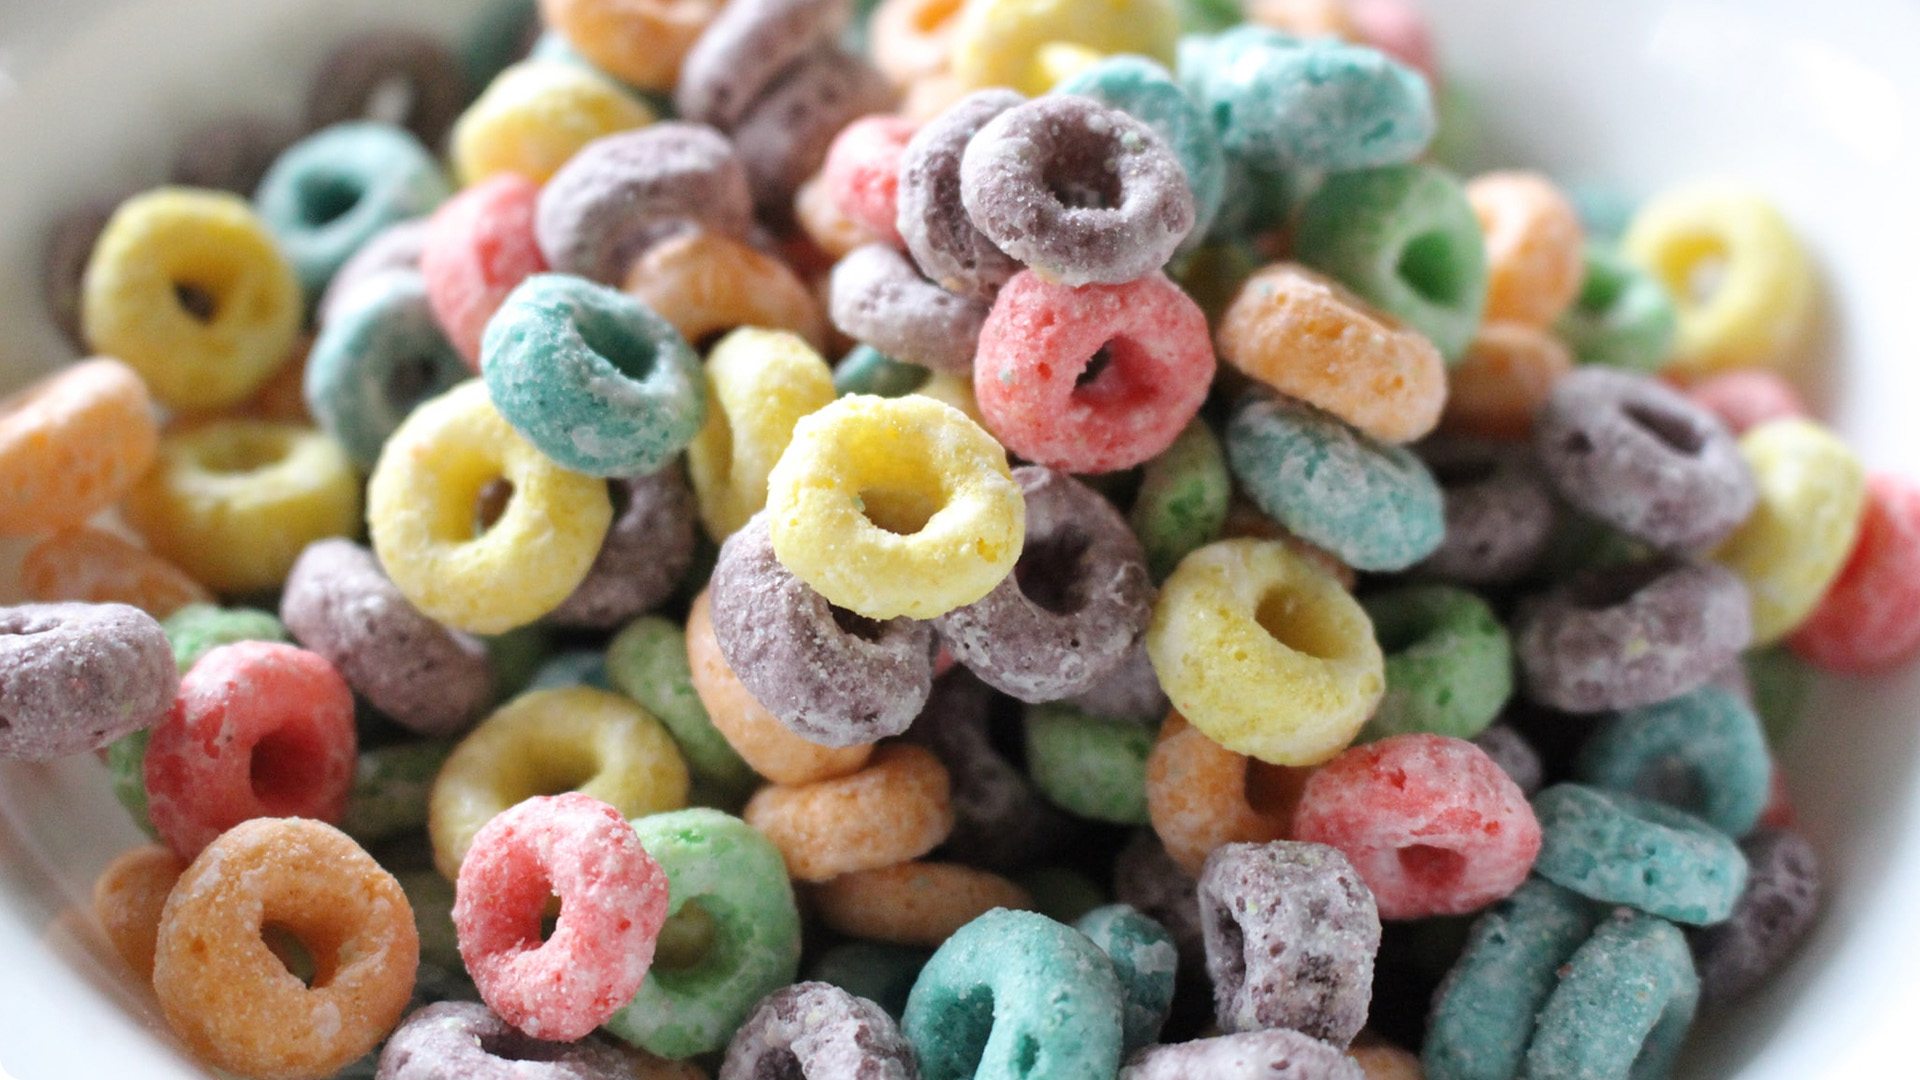
ROCOM delivers food-grade pneumatic conveying, sanitary vibrating screens, easy-clean magnetic separation, valves for flow control, big bag handling units or gravimetric dosing equipment. Systems can include food-contact stainless steel, smooth internal surfaces, reduced retention zones and easy-access or CIP-ready components.
Food & Dairy Handling Challenges
Food and dairy powder handling must control hygiene, product retention, allergens and combustible dust while maintaining reliable flow and accurate dosing. Key challenges include bacterial growth, cross-contamination, difficult cleaning, moisture sensitivity and dust emissions, requiring sanitary design, food-contact materials, easy-access or CIP-ready components and appropriate ATEX protection.
Hygiene & Compliance
Our approach considers EHEDG principles, FDA food-contact requirements, HACCP controls, ATEX food-powder risks and NFPA 652 combustible-dust guidance. The result is dependable powder handling from raw-material intake through conveying, screening, separation and dosing.
Our Bulk Handling Solutions for Food & Dairy
Conveying — Pneumatic, Vacuum & Mechanical
To transfer fragile milk powders and ingredients without degradation or environmental exposure, we utilize dense-phase pneumatic conveying and gentle vacuum conveying systems. Vacuum transport is inherently safer for explosive environments, as any leak draws air inward rather than blowing combustible dust out into the plant. For high-capacity ingredient transfer, our enclosed mechanical conveying lines ensure smooth, dust-tight transport.
Modular Piping & Flexible Connectors: Our process lines utilize food-grade, stainless-steel modular piping systems featuring quick-release clamps for rapid disassembly during Clean-In-Place (CIP) or Wash-In-Place (WIP) cycles. To isolate vibrating machinery while maintaining absolute containment, we integrate hygienic, flexible dust-tight connectors that eli
minate crevices where organic material could collect, spoil and harbor bacteria.
Hygienic Slide Gates, Rotary Valves & Diverters
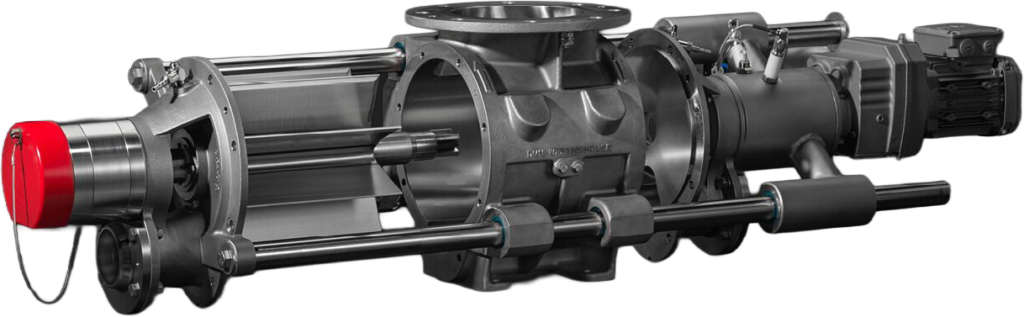
Engineered to prevent product entrapment, our ATEX-certified rotary valves feature support rails and quick-demount rotors, allowing operators to safely slide the rotor out for direct washing. Accompanying pneumatic slide gates and multi-port diverters feature mirror-polished internal surfaces and food-grade seals, ensuring positive material shut-off and stream diversion without dead zones.
Dust Filters & Industrial Vacuum Cleaners (ATEX)
To proactively eliminate the primary cause of secondary dust explosions, we supply specialized ATEX-rated vacuum industrial cleaners. These heavy-duty, grounded vacuum systems safely capture fugitive combustible food dust from floors, ledges and structural beams before it can pose a safety hazard.
Screening & Sieving — Sanitary Vibrating Screens
Positioned before mixing or directly ahead of packaging lines, our high-frequency vibrating screens gently sift out oversized agglomerates, foreign matter, and lumps caused by humidity, ensuring a perfectly uniform particle size while protecting recipe purity.
Weighing, Feeding & Dosing
High-Accuracy Weighing & Feeding Equipment: For strict nutritional compliance and recipe consistency, our gravimetric weighing & feeding equipment delivers split-second dosing accuracy. Built with fully welded, polished contact surfaces, these feeders prevent material build-up and are easily sanitized between product batches.
Magnetic Separation — Easy-Clean Drawer Magnets
To guarantee absolute consumer safety and protect downstream machinery, high-intensity, dairy-grade magnetic separators are integrated inline. Featuring easy-clean drawer designs, they continuously extract ferrous particles and scale from the ingredient stream.
Filling, Emptying & Packaging
Big Bag Filling & Emptying Units
Designed for sanitary bulk bag (FIBC) logistics, our emptying stations utilize inflatable, dust-tight docking seals to prevent fine powders from escaping during discharge. Active massage paddles gently break up bridging dairy powders, while our filling stations feature integrated load cells and automatic densification to pack bags cleanly, safely and accurately.
Dust-Controlled Loading Chutes
For high-volume shipping of flour, sugar or starches into bulk tankers, our telescopic loading chutes extend directly into the vehicle hatch. They use double-wall internal cones to separate the falling product from the exhaust air, utilizing negative-pressure dust extraction to keep the loading bay completely free of combustible dust risks.
Hygienic Packaging, Palletizing & Wrapping
Our automated packaging lines form, fill and seal finished food products into modified-atmosphere, moisture-barrier bags to preserve shelf life. These are transferred to high-speed palletizers that assemble perfectly square, stable stacks, followed by automated stretch-wrapping or stretch-hooding units that secure the loads with high-tension film for dust-free, hygienic transport and storage.
Food & Dairy Solutions
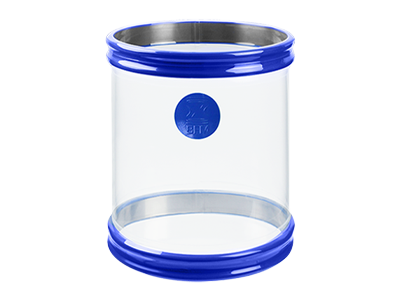
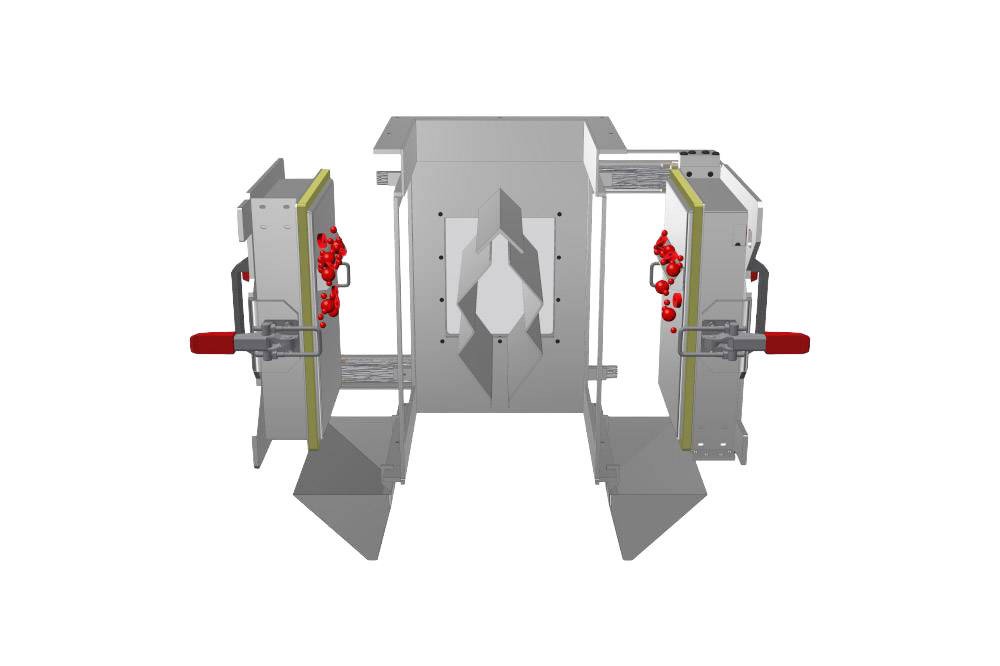
Bulk Handling Technologies for Food & Dairy
- Magnetic Separation Equipment
- Slide Gate Valves
- Rotary Valves
- Vibrating Equipment
- Weighing & Feeding Systems
- Dust Filters & Industrial Vacuum Cleaners
- Mechanical & Pneumatic Conveying
- Filling & Emptying Systems
- Loading Chutes
- Packaging, Palletizing & Wrapping Systems
Frequently Asked Questions
What is hygienic food powder handling?
Bulk material handling for food & dairy covers the systems that move, screen, dose, separate and package dry food powders — milk powders, infant formula, whey, sugars, starches and spices — to the highest sanitary standards. The equipment must be food-grade, easy to clean and ATEX-compliant to control combustible dust. ROCOM designs and integrates hygienic conveying, screening, weighing, dust-control and packaging systems for food and dairy producers.
How do you prevent contamination and allergen cross-contact?
With enclosed, dust-tight conveying, crevice-free hygienic design, quick-demount components for fast cleaning between products, magnetic separation and sieving to remove foreign bodies, and dust control to stop airborne cross-contamination.
Why is ATEX important when handling food powders?
Many food powders — milk powder, flour, sugar, starch — are combustible and can form explosive dust clouds. ATEX-rated conveying, vacuums, rotary valves and dust collection prevent ignition and protect people and the plant (NFPA 652 is the equivalent US standard).
Which food and dairy powders can ROCOM's systems handle?
Infant formula, milk and whey powders, sugars, starches, spices and other dry ingredients — including fragile, hygroscopic and cohesive powders that need gentle, controlled handling.
Our Partners

Contact Us
We look forward to discussing with you!